Custom 24VDC Pallet Transfer: High-Capacity Performance with Lower Control Costs
When a standard pallet conveyor configuration does not match the application, the right answer is not to force the fit. Material Handling Technologies (MHT) engineered a custom 24VDC pallet transfer for a customer that needed to handle loads up to 1,200 lbs. while meeting specific transfer and operating requirements.
Rather than defaulting to a typical AC/480V motor arrangement, MHT designed the system around the application’s load, speed, lift and control needs. The result is a custom pallet transfer conveyor that combines high-capacity pallet handling with a 24VDC motor driven roller (MDR) approach, helping reduce control-system costs without compromising the required performance.
Project at a Glance
| Specification | Project Detail |
| Capacity | 1,200 lbs. |
| Transfer Chain | No. 80 Flat Bar Chain |
| Chain Centers | 18″ |
| Chain Speed | 30 FPM |
| Lift | Positive Lift |
| Drive | (1) 2.5″ MDR Roller |
| Power / Controls | 24vDC |
The Challenge
The customer needed a pallet transfer solution capable of moving loads up to 1,200 lbs. at 30 FPM with reliable positive lift. The transfer also had to meet application-specific pallet handling requirements while avoiding unnecessary control-system cost and complexity.
An off-the-shelf pallet conveyor system was not the right fit. MHT’s engineering team evaluated the performance requirements and developed a custom conveyor system designed around the actual demands of the operation instead of applying a standard configuration.
The Custom 24VDC Pallet Transfer Solution
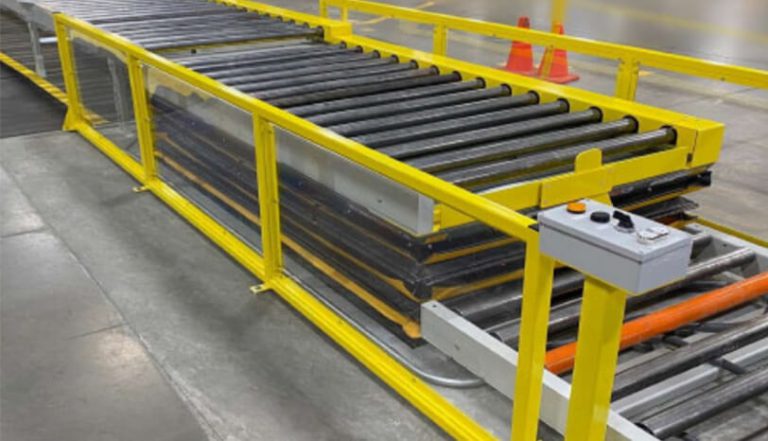
MHT designed the custom 24VDC pallet transfer with No. 80 Flat Bar Chain on 18-inch chain centers and a 30 FPM chain speed. The system uses positive lift to support controlled pallet transfer within the application.
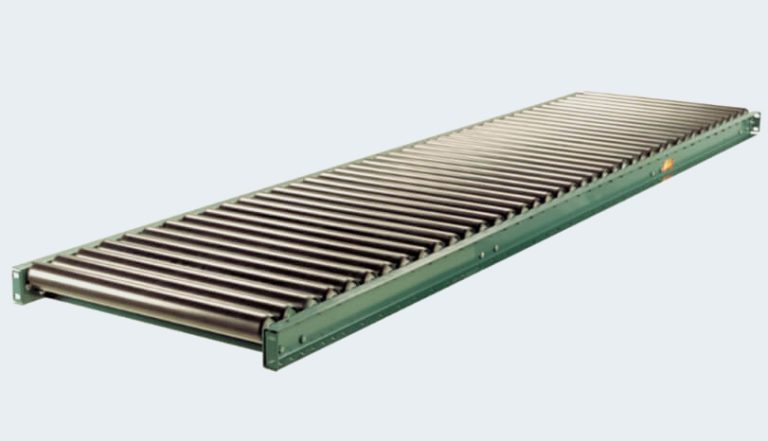
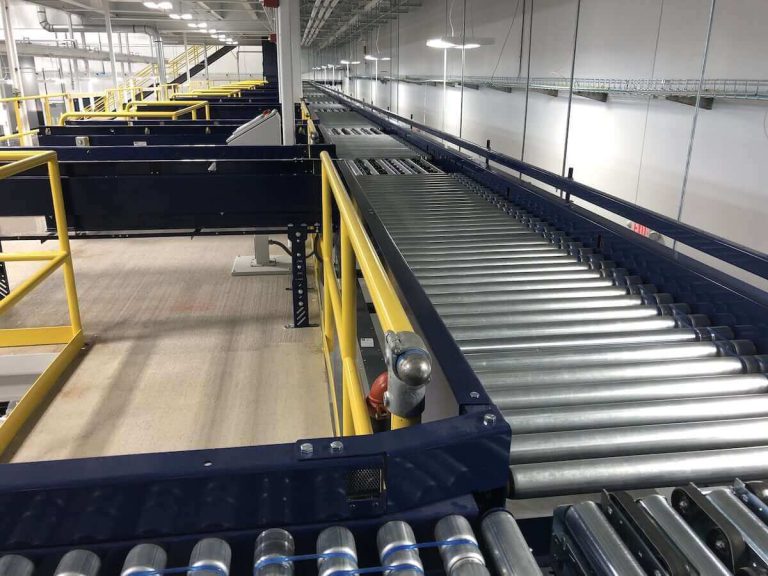
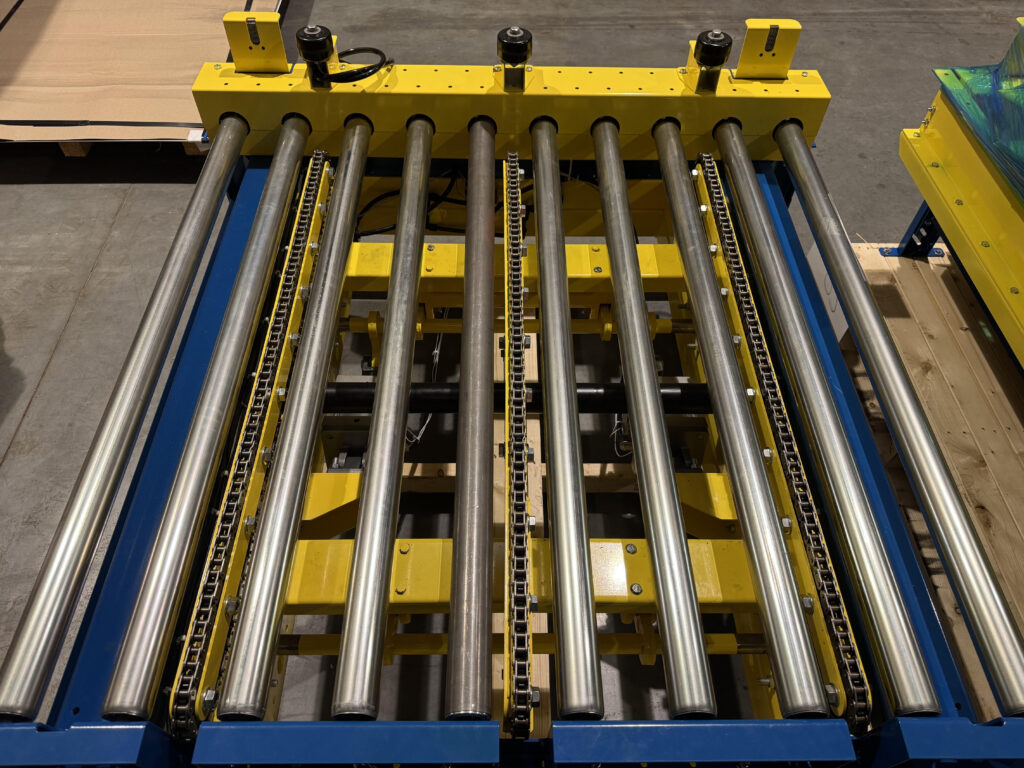
At the heart of the drive configuration is one 2.5-inch MDR roller. Positioned perpendicular to the other rollers, it uses three sprockets welded to the roller tube to drive the transfer chains. This tailored MDR pallet conveyor approach demonstrates how 24VDC conveyor technology can be applied beyond a standard conveyor layout to meet specific pallet-handling needs.
Engineering for Cost Efficiency
For this application, MHT selected 24VDC technology instead of a typical AC/480V motor configuration. That choice helped reduce control-system costs while still meeting the system’s 1,200-lb capacity, 30 FPM operating speed and positive-lift requirements.
The decision reflects MHT’s approach to custom material handling solutions: start with what the operation truly needs, then engineer the right combination of performance, controls and cost. A standard design is not automatically the most practical one, particularly when a custom solution can meet the application’s requirements more efficiently.
The Results
The completed system delivered a custom pallet transfer built for the application’s confirmed requirements:
- 1,200-lb load capacity
- 30 FPM chain speed
- Positive-lift pallet transfer
- MDR-based drive configuration
- Lower control-system costs compared with a typical AC/480V motor approach
By tailoring the system to a non-standard material handling requirement, MHT delivered a solution that met the required capacity and transfer performance while addressing control costs.
Custom Material Handling Solutions Built Around Your Operation
Not every challenge can be solved with standard conveyor equipment. MHT designs and integrates custom conveyor systems around each operation’s load requirements, speed, facility constraints and automation goals. From 24VDC pallet conveyor systems to broader automated material handling solutions, our team brings engineering, integration and project-management expertise together to help operations move materials more effectively.
For more on 24VDC/MDR technology, explore MHT’s StealthZone™ Pallet Conveyor or read our guide to 24 Volt DC MDR conveyors.